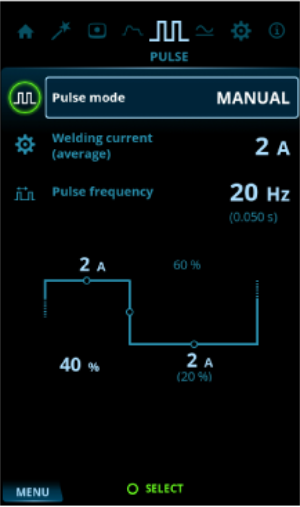
Pulse view
_400x170.png)
To adjust parameters:
| 1. | Go to the Pulse view. |
| 2. | Turn the control knob (1) to browse through the parameters. |
| 3. | Select a parameter for adjustment by pressing the control knob button (1). |
| 4. | Adjust the parameter by turning the control knob (1). |
| 5. | Close the parameter setting by pressing the control knob button (1). |
Adjustable parameters:
| Parameter | Value | Description |
|---|---|---|
| Pulse mode | OFF / Auto / Manual / Double | Pulse TIG: TIG welding process, where the welding current changes between two current levels: base current and pulse current. Parameters can be set either manually or automatically. Used for optimizing the arc characteristics for desired welding applications. In DC current mode: - When OFF is selected, pulse settings are not visible. - When Auto is selected, pulse settings are visible but not adjustable. - When Manual is selected, pulse settings are visible and adjustable. In AC current mode, only OFF or Manual can be selected. |
| Average current | Min = Current limit min Max = Machine-specific |
These values depend also on other pulse parameters. Maximum average current is also limited by the machine specifications. |
| Pulse frequency | 0.2 Hz ... 10 Hz, step 0.1 Hz, 10 Hz ... 300 Hz, step 1 Hz |
Determines how many pulse cycles are created per second (Hz). When AC current mode is used, the maximum pulse frequency is 20 Hz. When double pulse mode is used, the maximum pulse frequency is 30 Hz. |
| Pulse current | 10 A ... 300 A, step 1 A | The higher current level of the pulse cycle. In TIG welding, its main task is to create weld pool or increase the heat of the weld pool. These values depend also on other pulse parameters. Maximum pulse current is also limited by the machine specifications. |
| Pulse ratio | 10 % ... 70 %, step 1 % | Determines how big part of the whole pulse cycle time is spent on pulse current. |
| Pulse base current | 10 % ... 70 %, step 1 % | The lower current level of the pulse cycle. In TIG welding, its main tasks are to cool down the weld pool and to maintain the arc. |

|
Adjusting one pulse parameter value has an effect on the other values as well. |
| Welding processes and features |
